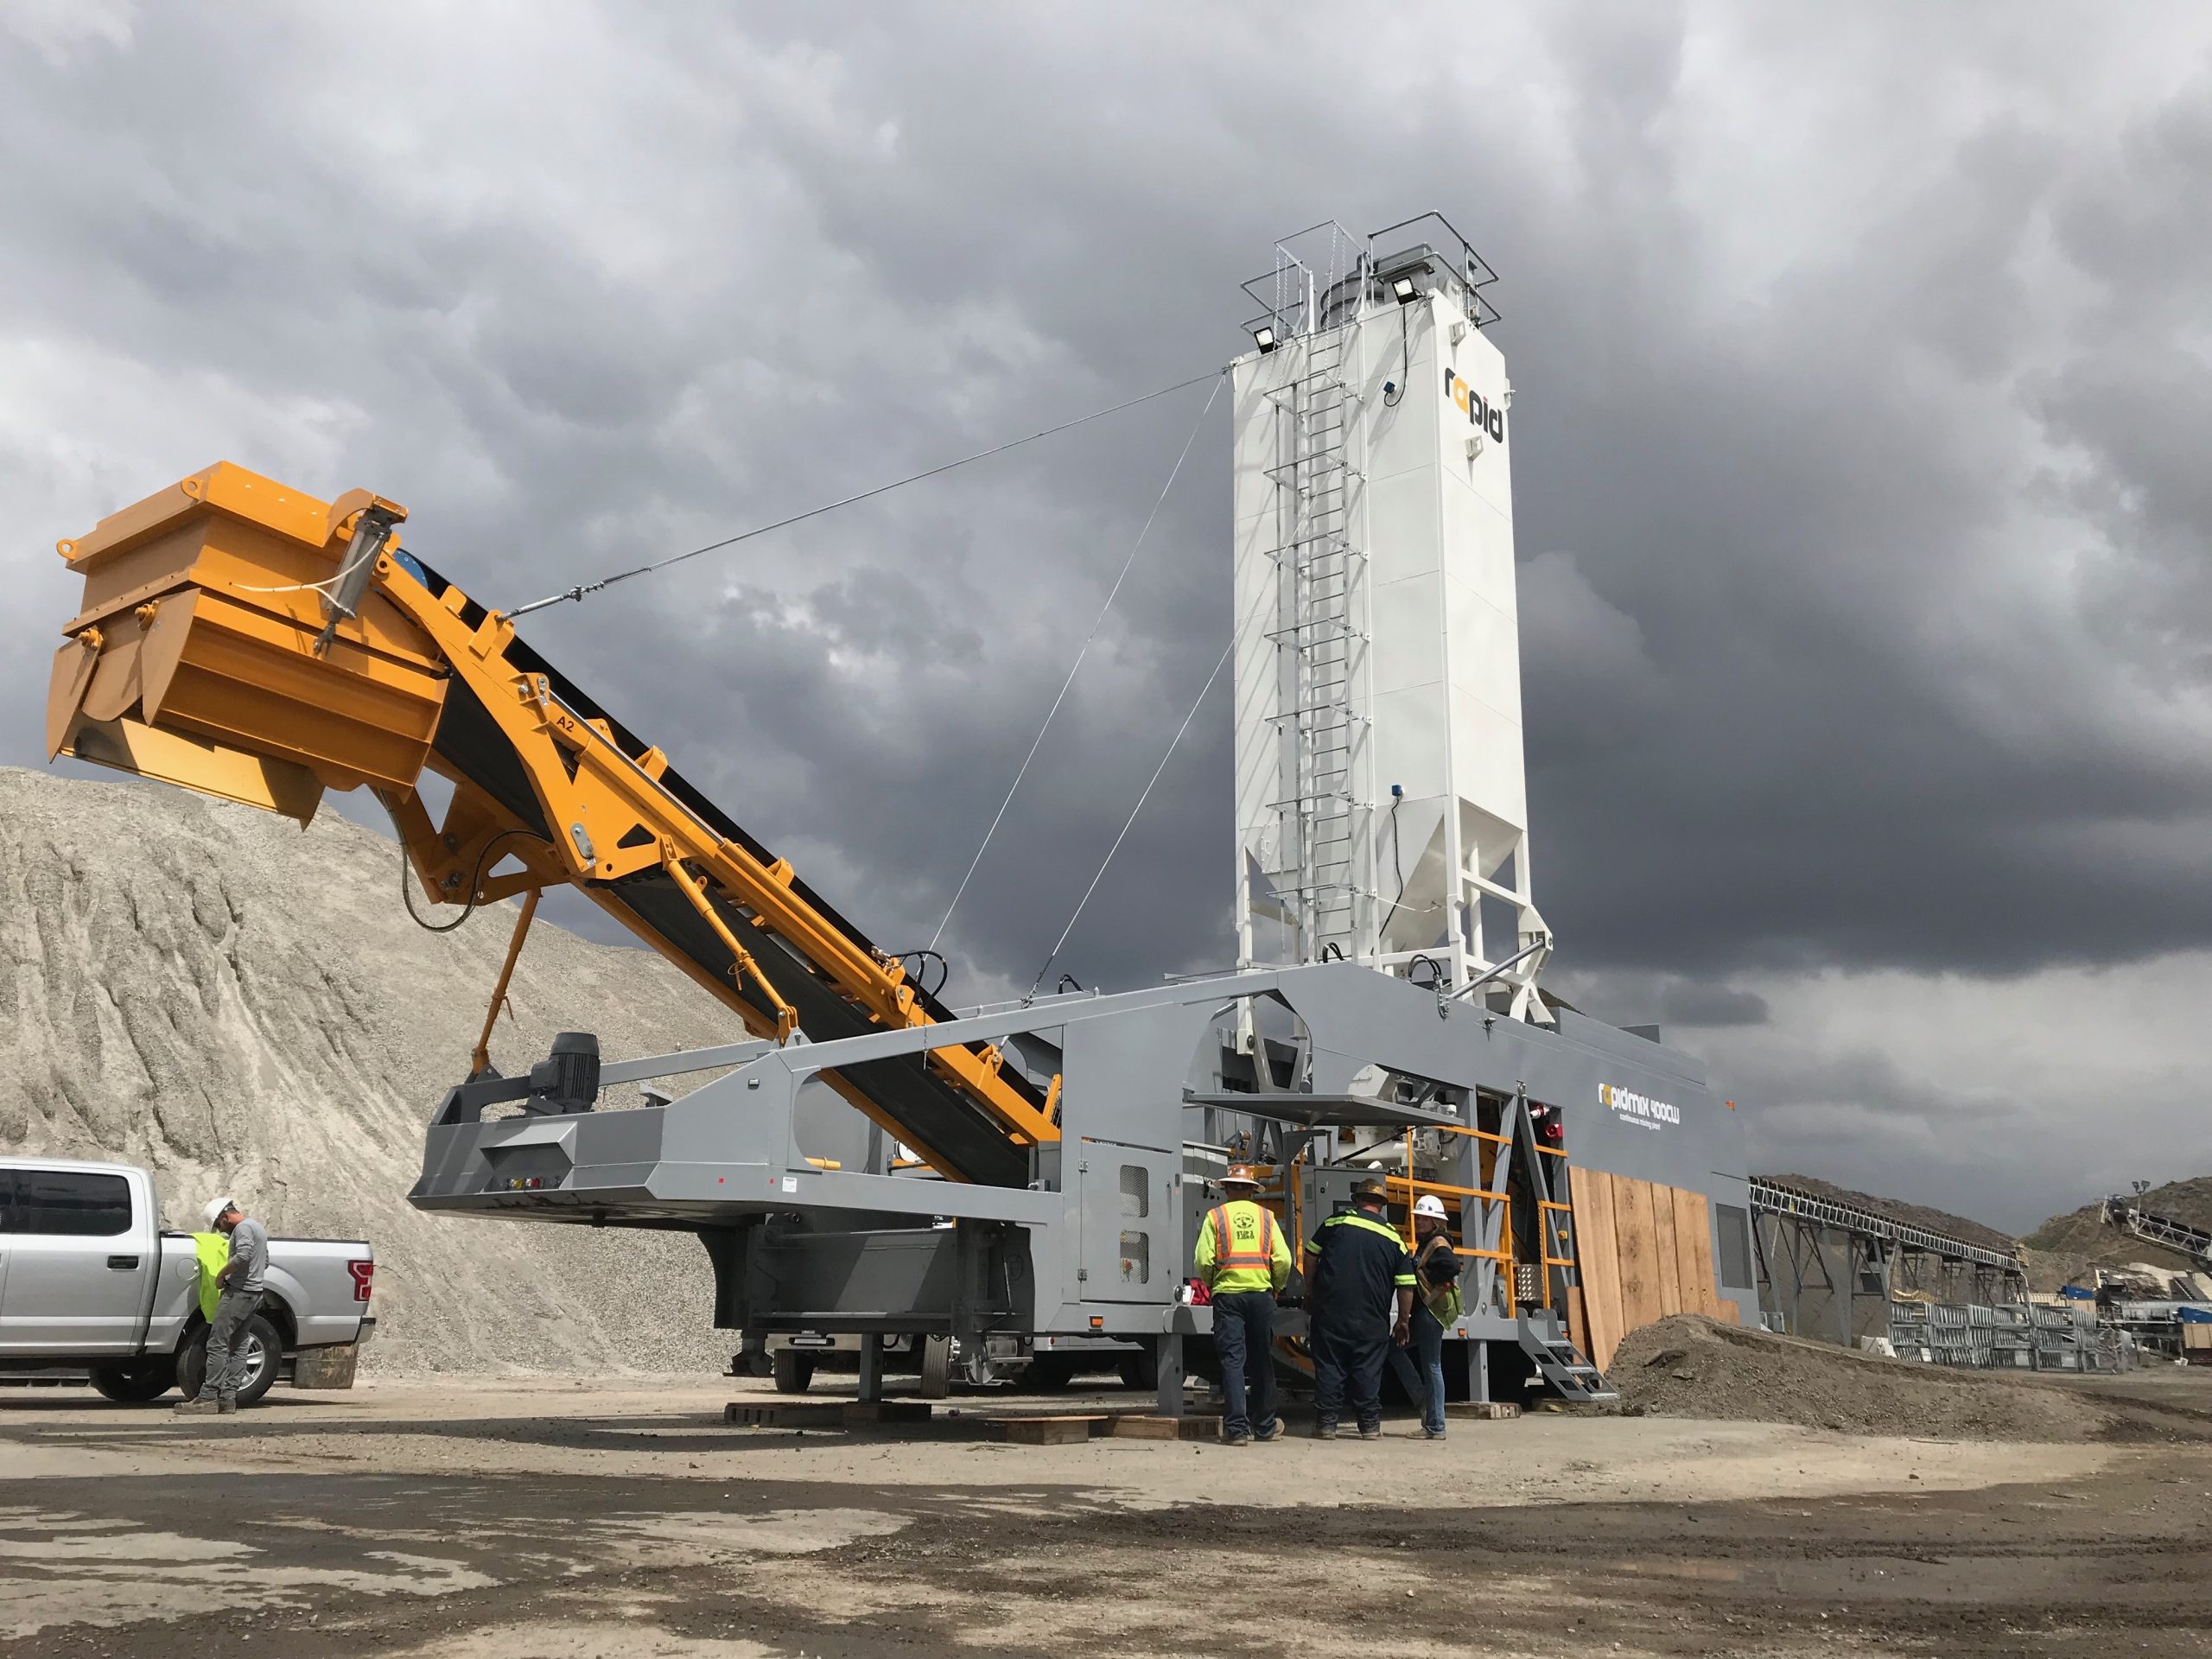
Pavement Recycling Systems chose to invest in a fully weighed Rapidmix 400CW mobile continuous mixing plant after a successful rental trial, using it to produce roller compacted concrete for a major port project and planning further use in the western US.
Introduction
Pavement Recycling Systems, a California company focused on pavement recycling and reclamation, needed a dependable mixing solution for their first roller compacted concrete project at a US port. Rapid International supplied a mobile mixing plant tailored to these needs.

The Problem
They required a mobile continuous mixing plant that could deliver consistent roller compacted concrete with precise weighing technology. The equipment also needed to be cost-effective and versatile enough for upcoming projects beyond the initial port work.
What Was Done
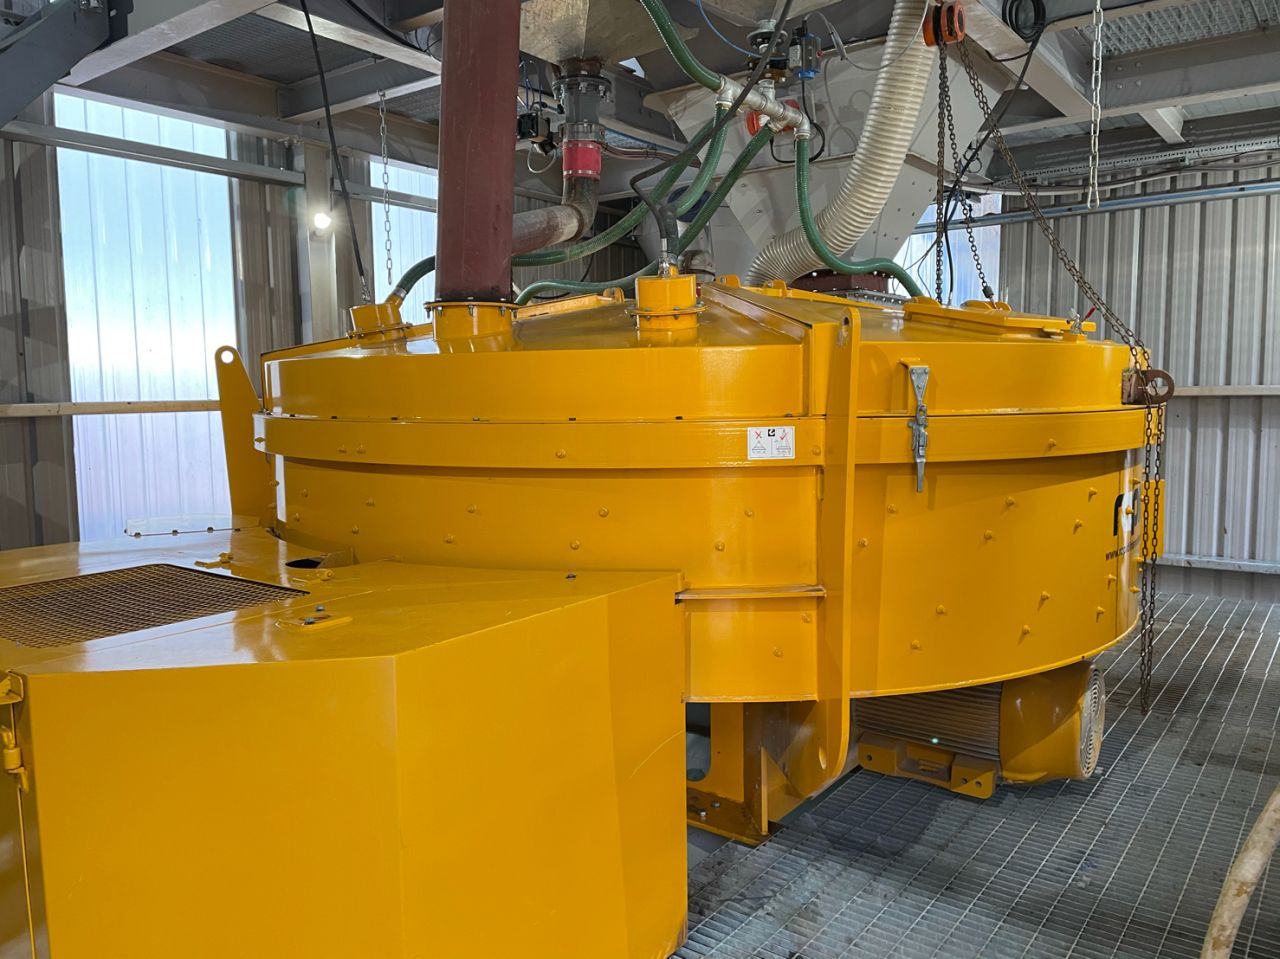
Pavement Recycling Systems started by renting a Rapidmix 400 mobile continuous mixing plant to test its performance. Impressed by the results, especially the weighing accuracy in newer models, they later purchased a fully weighed Rapidmix 400CW for their “Renew” division. This plant combines aggregates, cement, and water using onboard systems, producing a controlled mix ready for immediate laying and compaction on site.
Results
The Rapidmix 400CW enabled the production of high-quality roller compacted concrete that met strict project standards. Its mobility and advanced weighing system allowed for efficient, fast on-site mixing. Pavement Recycling Systems plans to use this equipment for more roller compacted concrete and other mixing tasks across California and the western states.
Closing Note
Thanks to its self-contained design and quick setup, the Rapidmix 400CW continues to provide a reliable and efficient solution for projects requiring accurate, high-volume mixing of semi-dry materials like roller compacted concrete.