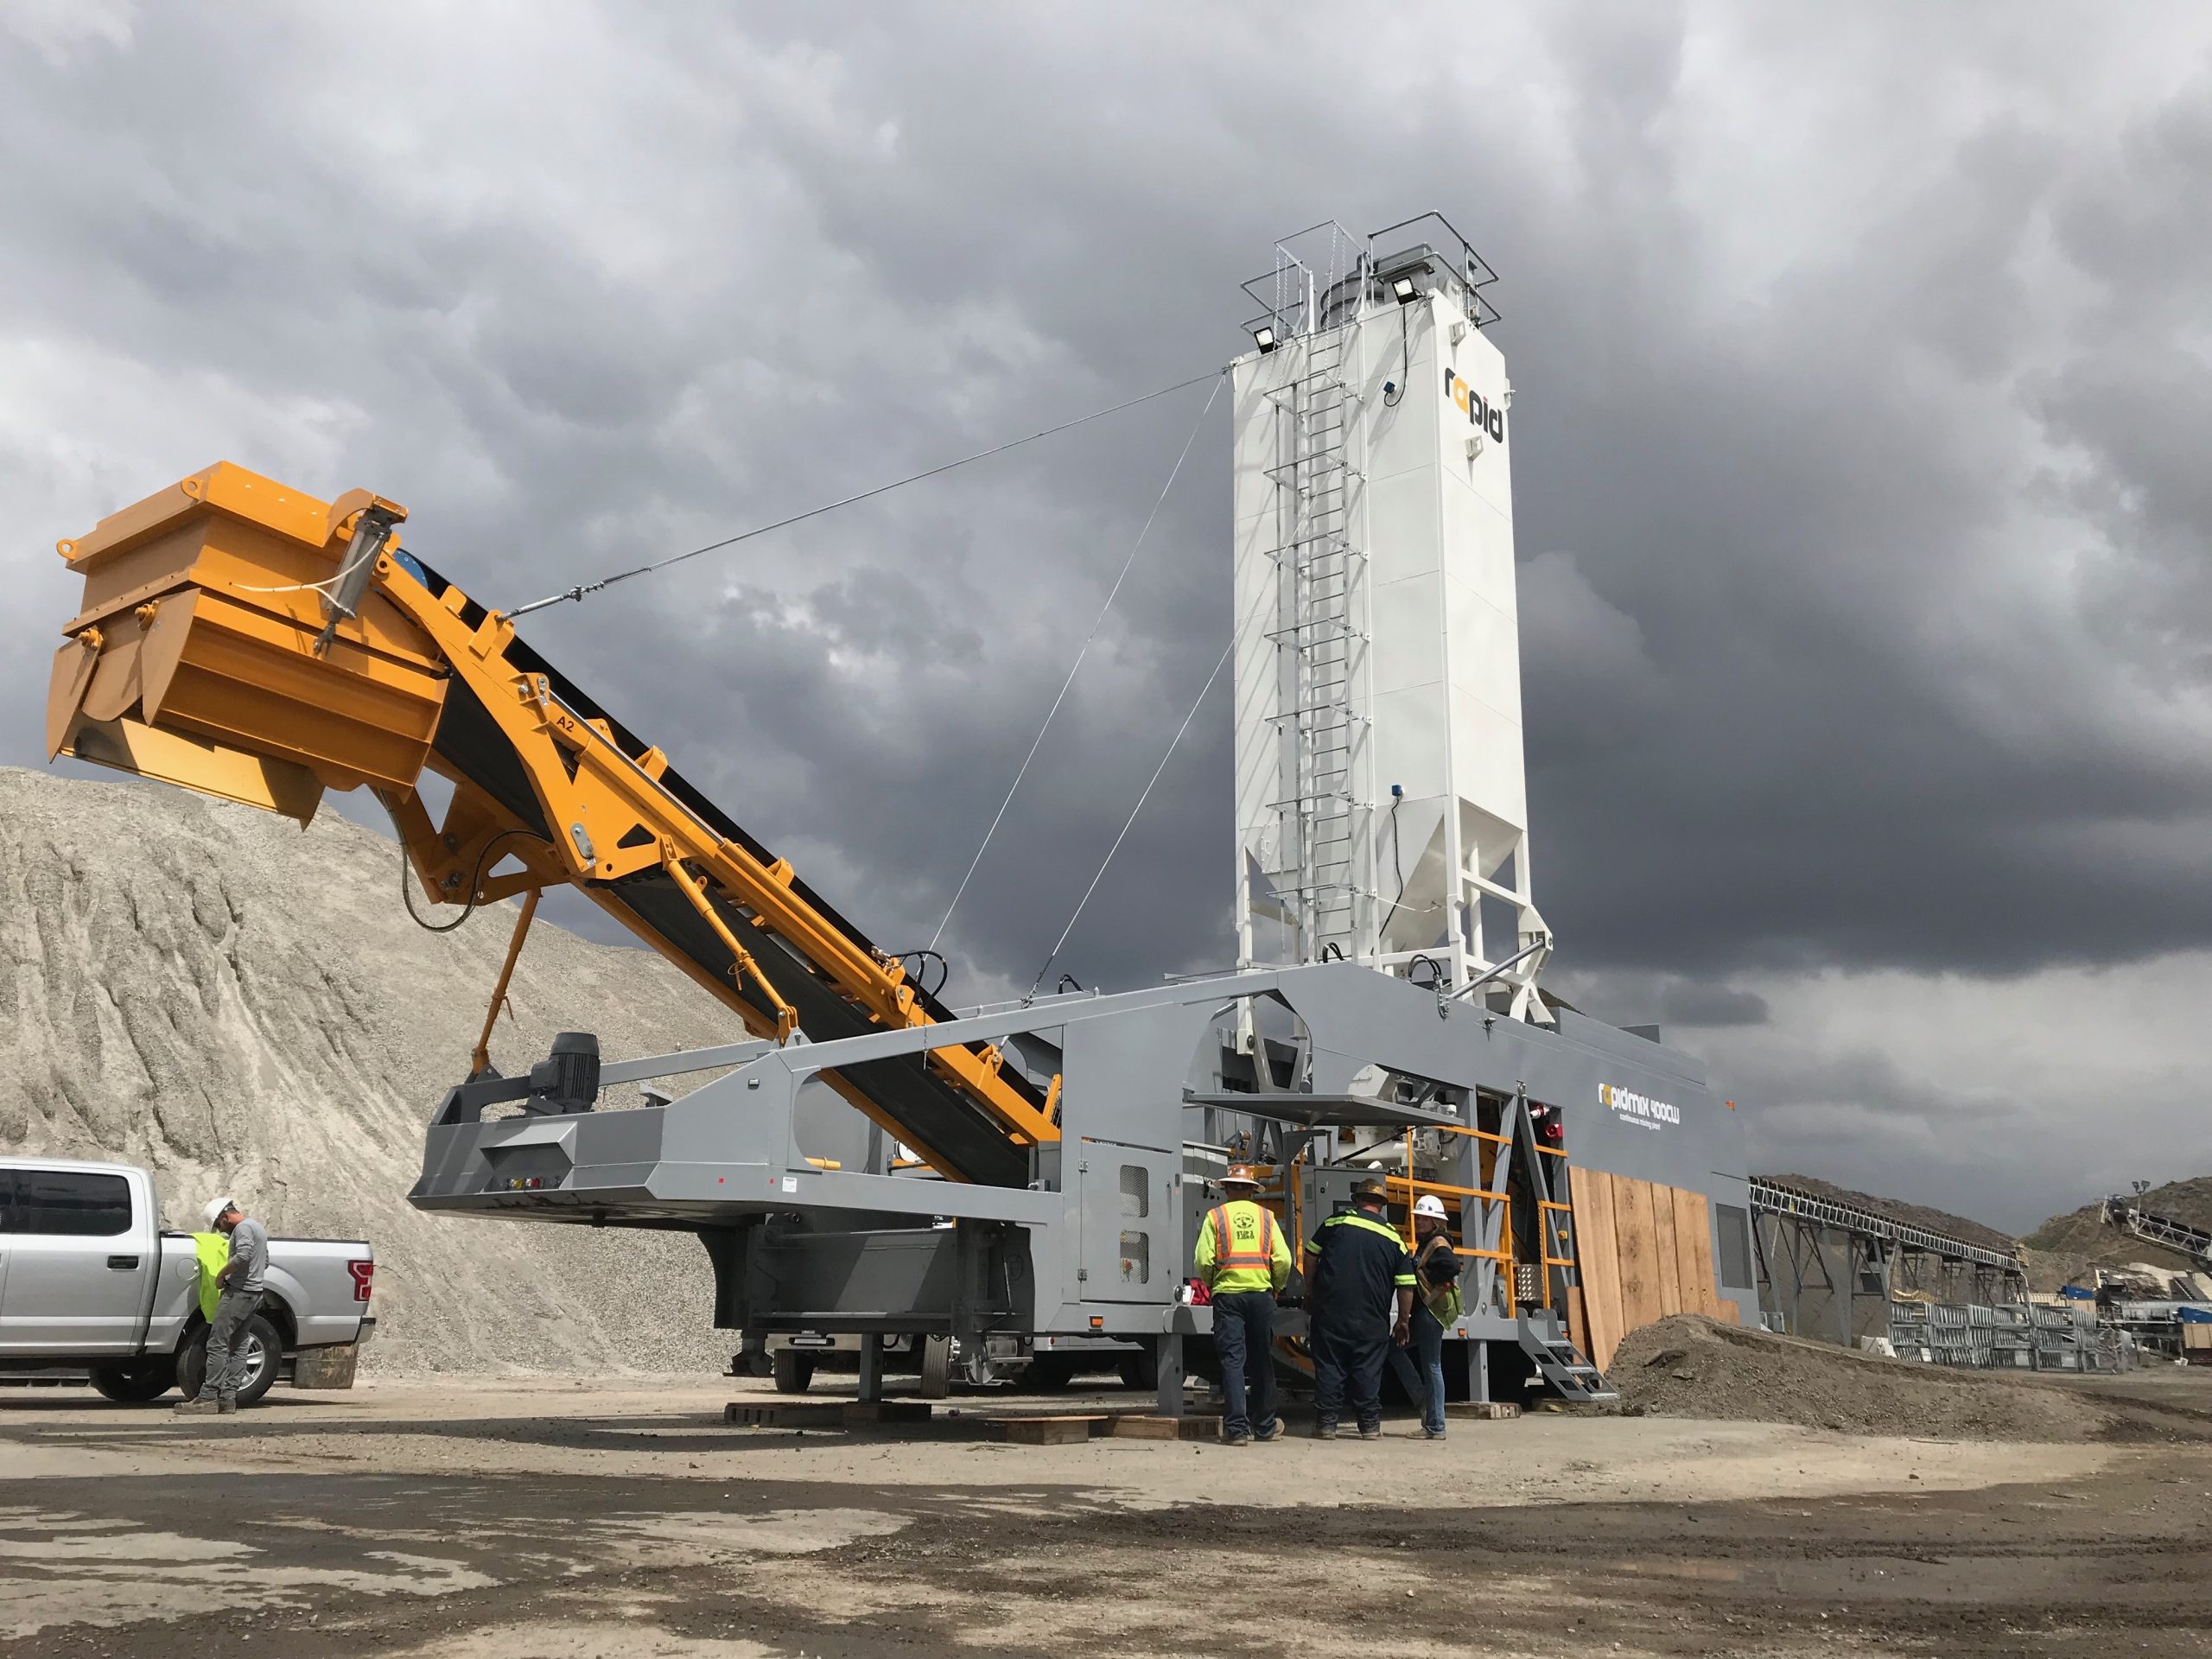
Allasso Recycling found the Rapidmix 400CW mobile continuous mixing plant to be the perfect fit for mixing bentonite enriched soils, thanks to its mobility, high capacity, and precise control.
Introduction
Allasso Recycling, a UK-based company specializing in recycling and construction, needed a reliable and efficient solution for producing bentonite enriched soils. These soils are used in landfill lining to create watertight barriers, requiring consistent mixing of bentonite, water, and host soil.

The Problem
The project involved covering a large area with a bentonite-enriched layer, which had to be carefully prepared in stages using two different types of host material with varying bentonite percentages. This complicated mixing process demanded a plant that could handle sticky, cohesive materials while maintaining accuracy and volume.
What Was Done
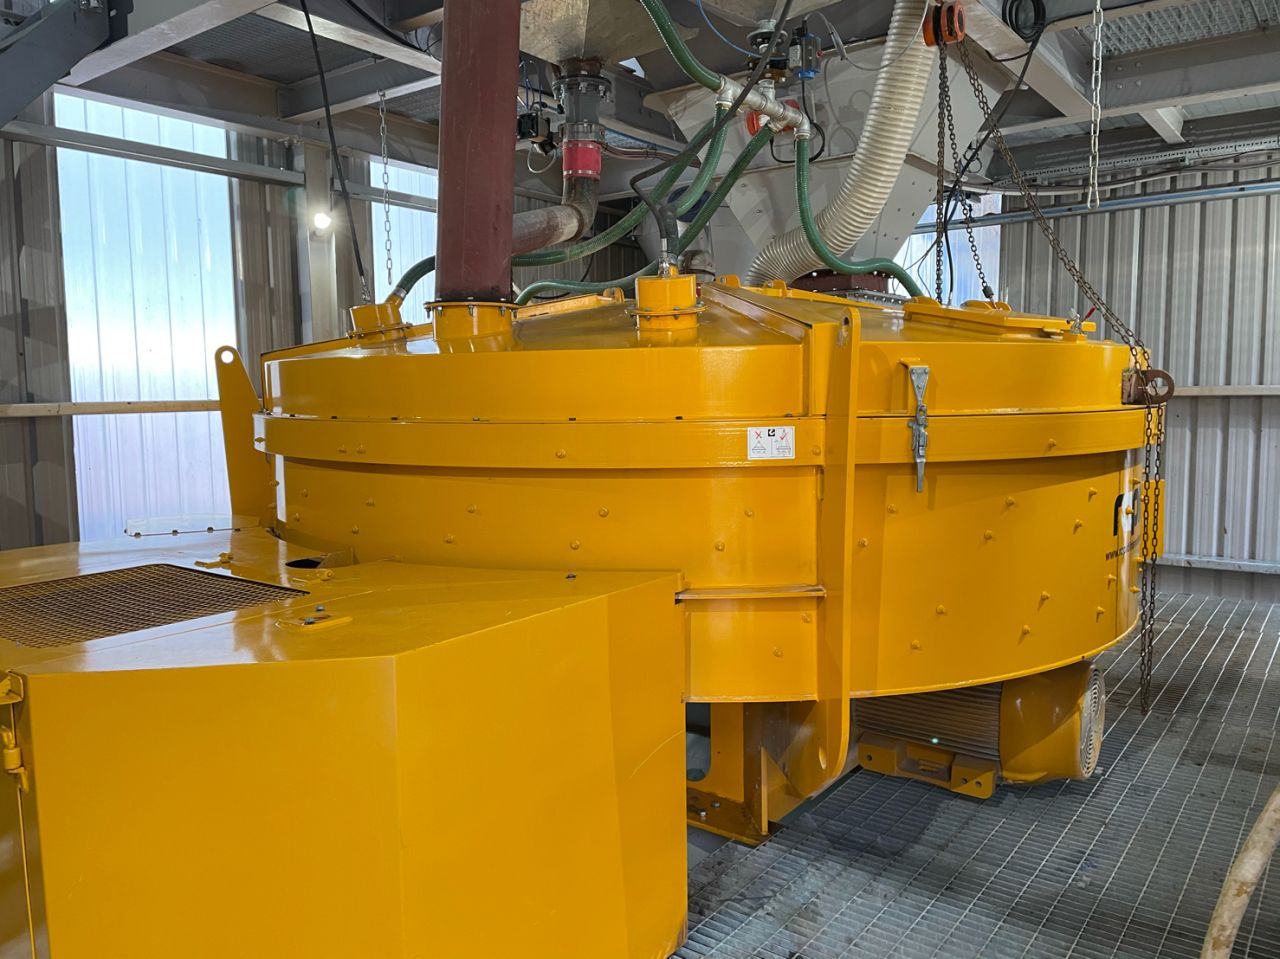
Allasso Recycling chose the Rapidmix 400CW, a self-contained mobile mixing plant known for its quick setup, high output, and advanced monitoring systems. Its design, including a clean-out belt that runs during mixing, helps handle the challenging properties of bentonite-enriched soils. The plant’s compact size and ease of movement made it ideal for working in tight spaces with phased construction.
Results
The Rapidmix allowed Allasso to produce large volumes of bentonite enriched soils with precise control over materials. Its mobility and reliability helped maintain production flow according to project needs. The company values the plant’s versatility and the support they receive from the Rapid team.
Closing Note
With features like full weighing of aggregates, cement, and water, along with a fast hydraulic setup, the Rapidmix 400CW delivers high-quality mixes efficiently on-site. It remains a trusted choice for civil engineering projects requiring both volume and precision.